| MOQ: | 1Ton |
| Price: | 800-1000 USD/Ton |
| Standard Packaging: | In bundles or in wooden boxes. |
| Delivery Period: | 20-30days upon products |
| Payment Method: | L/C, D/A, D/P, T/T |
| Supply Capacity: | 60000 Ton/Tons per Year |
![]()
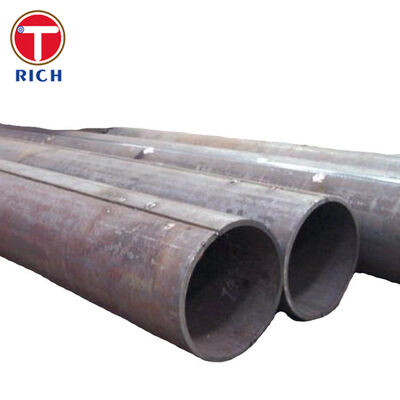
ASTM A672 electric-fusion-welded steel pipe is manufactured from pressure-vessel-quality steel plate using an electric-fusion welding process with filler metal. It is designed primarily for high-pressure service at moderate temperatures where large outside diameters, controlled mechanical properties, and verified weld integrity are required.
ASTM A672/A672M uses a Grade and Class designation system. The Grade identifies the pressure-vessel plate specification used for pipe manufacture, while the Class defines the pipe heat-treatment condition and whether radiographic examination and pressure testing are required. Common materials include ASTM A515 carbon steel plate grades and ASTM A516 fine-grain carbon steel plate grades.
The specification nominally covers electric-fusion-welded pipe with an outside diameter of 400 mm and larger and wall thicknesses up to 75 mm. Other dimensions can be manufactured when all applicable ASTM A672 requirements are satisfied.
| Item | Specification |
|---|---|
| Product | Electric-Fusion-Welded Steel Pipe |
| Standard | ASTM A672/A672M |
| Manufacturing Process | Electric-Fusion Welding with filler metal |
| Base Material | Pressure-vessel-quality carbon or alloy steel plate |
| Common Grades | B60, B65, B70, C60, C65, C70, D70 and other ASTM A672 grades |
| Common Classes | Class 10–13, 20–23, 30–33, 40–43, 50–53 |
| Outside Diameter | Nominally 400 mm and larger |
| Wall Thickness | Up to 75 mm |
| Length | 1–12 m, customizable according to project requirements |
| Pipe End | Plain end, beveled end or machined end |
| Dimensional Tolerance | According to ASTM A672/A672M and purchase specification |
| Straightness | Controlled according to applicable manufacturing and project requirements |
| Surface Condition | As-welded, shot blasted, bare, painted or coated as specified |
| Heat Treatment | None, stress relieved, normalized, normalized and tempered, or quenched and tempered depending on Class |
| Weld Examination | According to specified ASTM A672 Class |
| Pressure Test | According to specified ASTM A672 Class |
| Certification | EN 10204 3.1 / project-specific inspection documentation available |
ASTM A672 does not define the product only by material strength. Each pipe is ordered using a material grade together with a manufacturing class.
For example:
Grade B60 is manufactured from ASTM A515 Grade 60 pressure-vessel plate.
Grade B65 is manufactured from ASTM A515 Grade 65 plate.
Grade B70 is manufactured from ASTM A515 Grade 70 plate.
Grade C60 is manufactured from ASTM A516 Grade 60 fine-grain pressure-vessel plate.
Grade C65 is manufactured from ASTM A516 Grade 65 fine-grain pressure-vessel plate.
Grade C70 is manufactured from ASTM A516 Grade 70 fine-grain pressure-vessel plate.
This system allows material strength, heat treatment, weld examination and pressure testing to be specified separately according to the service conditions.
ASTM A672 pipe is produced by electric-fusion welding with filler metal. Weld quality can be verified by radiographic examination depending on the ordered Class.
Classes ending in 1 or 2, such as Class 11, 12, 21, 22, 31 and 32, incorporate radiographic examination requirements specified by ASTM A672.
This is particularly important for large-diameter pressure piping because the longitudinal weld becomes a critical pressure-retaining section of the pipe.
ASTM A672 provides specific Classes for different thermal conditions:
| Class Series | Heat Treatment |
|---|---|
| 10–13 | No pipe heat treatment |
| 20–23 | Stress relieved |
| 30–33 | Normalized |
| 40–43 | Normalized and tempered |
| 50–53 | Quenched and tempered |
The appropriate Class should be selected according to base plate grade, service temperature, design code and required mechanical properties.
Production testing includes tensile testing of finished pipe lots and transverse guided weld bend testing. The testing verifies both the mechanical properties of the pipe and the integrity and ductility of the welded joint.
Chemical analysis is also controlled for the pressure-vessel plate and deposited weld metal as required by the applicable specification.
A frequent procurement problem with ASTM A672 pipe is specifying only the grade while omitting the Class. The Class directly affects heat treatment, radiographic examination and hydrostatic testing.
We manufacture and document the product according to the complete designation requested in the purchase order, such as:
ASTM A672 B60 Class 12
ASTM A672 C60 Class 22
ASTM A672 C65 Class 22
ASTM A672 C70 Class 32
The Grade, Class, plate heat number, weld procedure, heat-treatment condition and inspection records can therefore be traced within the manufacturing documentation.
ASTM A672 requires pressure-vessel-quality plate rather than ordinary structural steel plate.
Plate materials can be controlled according to the designated ASTM plate specification, including ASTM A515/A515M, ASTM A516/A516M, ASTM A537/A537M and other materials permitted by ASTM A672.
Material certificates can identify:
Plate specification and grade
Heat number
Chemical analysis
Mechanical properties
Plate thickness
Heat-treatment condition
Pipe manufacturing batch
This provides traceability between incoming pressure-vessel plate and finished EFW pipe.
Different projects require different levels of weld inspection and pressure verification. ASTM A672 allows these requirements to be defined through the Class designation rather than applying the same inspection configuration to every pipe.
For example:
| Class | Heat Treatment | Radiography | Pressure Test |
|---|---|---|---|
| 10 | None | No | No |
| 11 | None | Yes | No |
| 12 | None | Yes | Yes |
| 13 | None | No | Yes |
| 20 | Stress relieved | No | No |
| 21 | Stress relieved | Yes | No |
| 22 | Stress relieved | Yes | Yes |
| 23 | Stress relieved | No | Yes |
| 30 | Normalized | No | No |
| 31 | Normalized | Yes | No |
| 32 | Normalized | Yes | Yes |
| 33 | Normalized | No | Yes |
| 40 | Normalized and tempered | No | No |
| 41 | Normalized and tempered | Yes | No |
| 42 | Normalized and tempered | Yes | Yes |
| 43 | Normalized and tempered | No | Yes |
| 50 | Quenched and tempered | No | No |
| 51 | Quenched and tempered | Yes | No |
| 52 | Quenched and tempered | Yes | Yes |
| 53 | Quenched and tempered | No | Yes |
This allows the inspection scope to be matched accurately to pressure-system design and project specifications.
| Standard | Description |
|---|---|
| ASTM A672/A672M | Electric-fusion-welded steel pipe for high-pressure service at moderate temperatures |
| ASTM A20/A20M | General requirements for steel plates for pressure vessels |
| ASTM A515/A515M | Carbon steel pressure-vessel plate for intermediate- and higher-temperature service |
| ASTM A516/A516M | Carbon steel pressure-vessel plate for moderate- and lower-temperature service |
| EN 10217-5 | Submerged arc welded steel tubes for pressure purposes |
| JIS G3456 | Carbon steel pipes for high-temperature service |
| GOST 10706 | Longitudinal electric-welded steel pipes |
| GB/T 9711 | Steel pipe for pipeline transportation systems |
The EN, JIS, GOST and GB standards listed above are procurement references for related pressure or welded-pipe products and should not be considered direct material equivalents to ASTM A672. Material substitution should be approved according to the engineering design code and project specification.
ASTM A672 electric-fusion-welded steel pipe can be used as a large-diameter main steam distribution header in industrial boiler and process utility systems.
For this application, the pipe carries pressurized steam between the steam-generation system and downstream process equipment. Material grade, wall thickness, heat treatment, weld examination and pressure testing should be selected according to the design temperature, design pressure and applicable piping code.
The following table shows representative heat-analysis requirements for five commonly specified ASTM A672 grades. ASTM A672 grades derive their chemical requirements from the corresponding pressure-vessel plate specification.
Values are weight percent. Carbon limits shown below are based on plate thickness not exceeding 25 mm unless otherwise stated.
| ASTM A672 Grade | Corresponding Plate | C Max. % | Mn % | P Max. % | S Max. % | Si % |
|---|---|---|---|---|---|---|
| B60 | ASTM A515 Gr.60 | 0.24 | 0.90 max. | 0.025 | 0.025 | 0.15–0.40 |
| B65 | ASTM A515 Gr.65 | 0.28 | 0.90 max. | 0.025 | 0.025 | 0.15–0.40 |
| B70 | ASTM A515 Gr.70 | 0.31 | 1.20 max. | 0.025 | 0.025 | 0.15–0.40 |
| C60 | ASTM A516 Gr.60 | 0.21 | 0.60–0.90 | 0.025 | 0.025 | 0.15–0.40 |
| C65 | ASTM A516 Gr.65 | 0.24 | 0.85–1.20 | 0.025 | 0.025 | 0.15–0.40 |
| ASTM A672 Grade | Corresponding Plate Grade | Tensile Strength MPa | Yield Strength Min. MPa | Elongation in 50 mm Min. |
|---|---|---|---|---|
| B60 | ASTM A515 Gr.60 | 415–550 | 220 | 25% |
| B65 | ASTM A515 Gr.65 | 450–585 | 240 | 23% |
| B70 | ASTM A515 Gr.70 | 485–620 | 260 | 21% |
| C60 | ASTM A516 Gr.60 | 415–550 | 220 | 25% |
| C65 | ASTM A516 Gr.65 | 450–585 | 240 | 23% |
![]()
![]()
![]()
![]()
A: manufacturer,also can do trading.
A: Generally speaking,it is 10-15 days if the goods are in stock,or it is 30-40 days if the goods are not in stock, it is according to quantity.
A: Yes, we could offer the sample for free charge but need pay the cost of freight.
A: Payment<=2000USD, 100% in advance. Payment>=2000USD, 30% T/T in advance ,balance before shippment.
If you have another question, pls feel free to contact with me.